
Custom Rubber Parts Manufacturers: Why Do Rubber Isolator Sleeves Become Brittle and Snap Easily?
Custom Rubber Parts Manufacturers: Why Do Rubber Isolator Sleeves Become Brittle and Snap Easily?
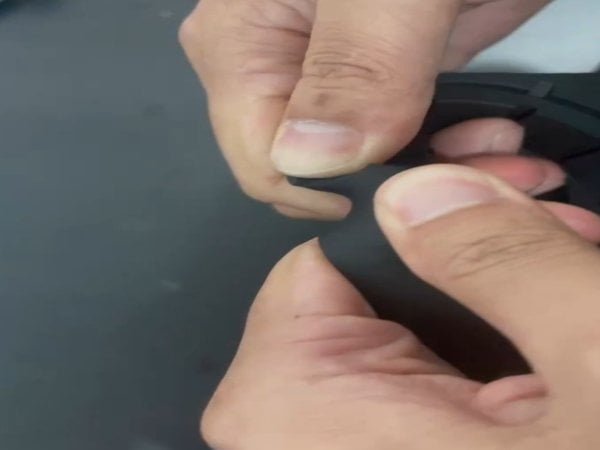
Discovering that delivered rubber vibration isolator sleeves lack structural strength and snap easily by hand?
This severe structural brittleness destroys equipment shock absorption and ruins client trust. Today, I am recording a real factory report detailing how a manufacturer resolved rubber sleeve brittleness and notch defects.
Rubber isolator sleeve snapping stems primarily from insufficient initial vulcanization time, combined with sharp mold groove edges that cause demolding strain. The manufacturing factory saved product quality by rounding mold sharp corners, mandating a 2-to-3-hour cooling period before flash tearing, and locking parameters in molding operation instruction sheets.
Why Do Insufficient Vulcanization and Sharp Mold Corners Cause Brittle Snapping in Custom Made Rubber Parts?
Insufficient vulcanization time prevents rubber polymer chains from cross-linking completely.
Under-cured polymer structures exhibit low tensile strength and become brittle upon demolding.
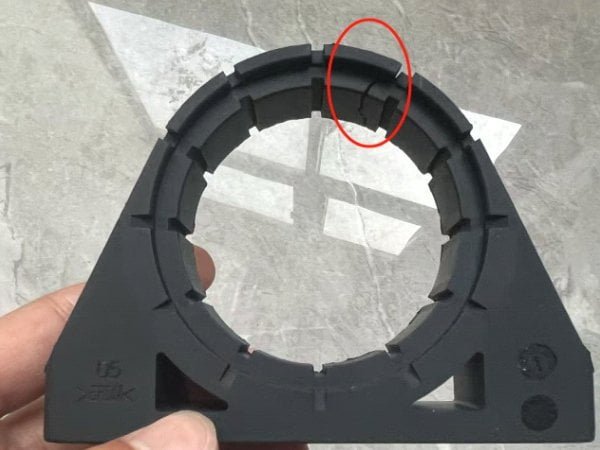
This factory report shows that the client reported insufficient body strength on rubber isolator sleeves, with notches along the edges, making them easy to snap by hand.
Upon receiving the report, the factory technical team launched troubleshooting immediately. Field audits confirmed 0 PCS in warehouse stock, 0 PCS in progress, and 0 PCS in transit. To resolve the issue completely, the factory arranged custom material compounding and re-scheduled production for 200 PCS.
The factory engineering team analyzed the root causes deeply and identified three primary factors.
First, the molding process followed parameters from initial trial physical property reports, where vulcanization time was insufficient, leaving parts under-cured and brittle upon demolding.
Second, mold groove edges were designed too sharp and straight, creating micro-tear cracks when parts experienced stress during demolding.
Third, post-processing operators tore off flash immediately while parts were hot right out of the mold, concentrating tearing forces at sharp notch points and tearing the rubber body. When manufacturing demanding custom made rubber parts, complete vulcanization and smooth mold radii determine tear resistance lifespan.
| Defect Physical Appearance | Root Cause Generation (Factory Analysis) | Physical & Material Mechanism | Factory Corrective Action |
|---|---|---|---|
| Brittle Body & Easy Snapping | Insufficient vulcanization time; under-cured | Low polymer cross-linking; tensile strength dropped | Adjusted vulcanization time; locked molding SOP |
| Micro Cracks & Edge Notches | Mold groove edges designed sharp & straight | Stress concentration during demolding caused tears | Repaired mold; rounded straight groove edges |
| Trimming Tear Damage | Flash torn manually while hot out of mold | Hot tear strength low; tearing damaged sleeve body | Mandated 2-to-3-hour room temp cooling period |
How Do Custom Rubber Parts Manufacturers Eliminate Sleeve Snapping via 3 Key Actions?
Hot rubber parts right out of the mold possess extremely low tear strength. Tearing flash without cooling causes notches regardless of material quality. The factory had to address cooling, mold rounding, and parameter locking simultaneously.
Professional custom rubber parts manufacturers establish strict post-processing protocols. The factory mandated a 2-to-3-hour cooling period after demolding before trimming, repaired molds to eliminate sharp corners, and drafted operation instruction sheets, successfully delivering 200 re-produced pieces after 100% inspection pass rates.
Factory Corrective Actions and 200 PCS Re-Production Verification Results
To resolve body brittleness and edge notches, the factory's quality improvement team implemented three corrective actions.
First, the factory updated the post-processing SOP workflow. The factory mandated that demolded parts must sit at room temperature for 2 to 3 hours to cool down, allowing rubber to recover optimal room-temperature tear strength before post-processing staff tear off flash.
Second, the engineering department issued a mold repair order to grind and round sharp groove edges, ensuring smooth demolding without scratching the rubber body.
Third, the quality and engineering departments jointly drafted molding inspection operation instruction sheets. The SOP clearly specified optimal vulcanization temperatures, curing times, and operational precautions, strictly forbidding staff from modifying parameters privately.
The silicone and rubber raw materials used by the factory comply with FDA Food Contact Regulations 및 RoHS Environmental Directives. The factory enforces quality controls under ISO 9001 Quality Standards. the factory re-produced 200 PCS, which passed 100% QC inspection for tensile strength and visual appearance before successful delivery.
| Verification Item | Detailed Engineering Standard & Execution | Actual Confirmation & Results |
|---|---|---|
| Demolding Cooling SOP | Force 2-to-3-hour room temp cooling before trimming | Hot tear damage avoided; notch defect rate 0% |
| Molding Mold Repair | Grind & round sharp mold groove edges | Smooth demolding achieved; micro-cracks eliminated |
| SOP Parameter Locking | Drafted Molding Operation Instruction Sheets | Complete cross-linking; elasticity & strength restored |
| 200 PCS Re-Production QC | Re-produced 200 PCS; 100% QC tensile & visual check | 100% qualified; client acceptance approved |
Summarizing this factory report, adequate vulcanization cross-linking time, smooth demolding structures, and proper cooling post-processing are cornerstones for guaranteeing rubber isolator sleeve tensile strength. Through process locking and mold repairs, the factory successfully resolved the snapping crisis.
How to Specifically Operate with custom rubber parts manufacturers?
When executing processes and quality systems with custom rubber parts manufacturers, factories must follow standardized procedures. Third-party testing data shows that using adequate vulcanization cross-linking time and high-temperature rubber processes, combined with 2-hour demolding cooling post-processing, keeps tensile strength at high levels and achieves 100% outgoing quality.
- Anomaly Audit & Re-Production: Confirm stock and in-transit items immediately upon complaint, arranging custom compounding and re-producing 200 PCS.
- Mold Sharp Corner Grinding & Rounding: Issue mold repair orders to round sharp groove edges, optimizing draft angles to eliminate stress points.
- 2-to-3-Hour Demolding Cooling SOP: Enforce a mandatory 2-to-3-hour room temperature cooling period after demolding before trimming operations start.
- Draft Vulcanization SOPs & 100% QC Check: Draft Molding Operation Instruction Sheets to lock parameters, performing 100% QC inspections on re-produced batches.
External References & Industry Citations
- ISO 9001 Quality Certification: ISO 9001 Quality Management Systems Standard
- FDA Food Contact Regulations: U.S. FDA 21 CFR 177.2600 Food Contact Safety Regulations
- RoHS Environmental Directives: European Commission RoHS Directive 2011/65/EU
About Me and Dibo Tech
Brand Name: Dibo Tech
Slogan: Dibo Technology Silicone Manufacturing Specialists
Website: https://samxine.com/
Our Mission:
Grounded in strong technical capability and quality, we specialize in custom OEM and ODM silicone rubber production, offering reliable custom solutions for our clients while fulfilling social responsibility for a sustainable future.
About Me:
My name is Kunfa Ye, but my friends call me Jeff. I was born in 1986 under the sign of the Tiger. I started working in the silicone rubber manufacturing industry in 2014, and I now have fifteen years of experience. Over these years, I started from scratch and experienced every rise and fall in manufacturing. I know the hardships and rewards of entrepreneurship deeply. I always focus on professionalism and integrity in every project.
The silicone manufacturing industry seems ordinary, but it affects every part of industrial production. I know that trust stands behind every product, and trade relies on mutual success. Over the years, my proudest achievement is not achieving personal financial independence, but helping my clients optimize their supply chains and improve production efficiency. Their success brings me far more joy than personal achievements.
Now, I hope to give back to the industry—sharing experience, answering questions, and connecting resources. Whether you are a startup or an experienced industry peer, if I can help, I will do my absolute best. Because I always believe: the essence of business is the transfer of value, and true fulfillment comes from how much help you can bring to others.