

Magnetic Silicone Balls: 5 Proven Steps to Fix Adhesive Defects
Magnetic Silicone Balls: How to Fix Adhesive Defects in Custom Magnetic Silicone Balls?
De-bonding leaks on delivered magnetic silicone balls?
Non-conforming items destroy client trust and trigger replacement expenses. I solve this technical defect using a real gluing process case study.
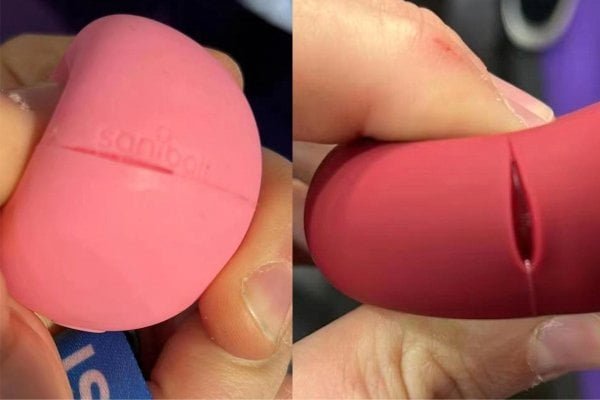
Fixing adhesive defects in Magnetic silicone balls requires stable dispenser air pressure and strict sampling. We installed air boosters on automatic dispensers to stabilize air pressure, eliminating glue volume surges. Meanwhile, we tightened OQC sampling AQL standards from MA:0.65 / MI:1.0 to MA:0.4 / MI:0.65, stopping defect outflows completely.
Many buyers and quality engineers feel confused when facing de-bonding complaints. Read on as I share our complete journey from complaint handling to hardware upgrades and quality tightening.
Why Do Unstable Dispenser Pressure and Low OQC Sampling Ratios Cause Magnetic Silicone Balls De-Bonding?
Broken glue beads allow de-bonding defects to slip out with bulk shipments.
This creates high replacement and logistics expenses. Proper air supply and sampling defense lines safeguard product quality.
Air pressure drops cause dispenser needles to extrude glue unevenly, creating voids on Magnetic silicone balls seam faces. If the OQC sampling ratio is too small without peel tests, minor de-bonding slips through to clients.

Pressure Fluctuation and Interception Gap Analysis
In my fifteen years of silicone manufacturing experience, I have handled many adhesion anomalies.
A client reported that previously delivered 2,000PCS magnetic silicone balls exhibited de-bonding and adhesive defects. I assisted the client in sorting the 2,000PCS batch immediately while arranging full replenishment.
Meanwhile, I audited our 20PCS warehouse stock, confirming 1PCS defective item, with 0PCS in transit for this model.
To locate root causes, I led my team in a deep teardown. We identified two primary causes.
First, main air line pressure fluctuations caused uneven glue output, leaving voids.
Second, the OQC sampling ratio was too small to intercept minor glue gaps.
We executed a horizontal audit across all similar silicone und custom silicone parts warehouse stock, eliminating potential risks.
| Failure & Outflow Dimension | Pre-Improvement Production & QC | Physical Mechanism & Hidden Risk | Resulting Impact |
|---|---|---|---|
| Dispenser Air Supply Pressure | Direct main air line supply; fluctuating | Pressure drops thin or break glue beads | Voids created on seam faces; de-bonding occurs |
| OQC Sampling Ratio | Small sampling ratio; visual checks | No seam peel tests performed; gaps missed | Defective items slip out; triggers complaints |
| Stock Audit Scope | Audited complaint batch only | No horizontal audit performed on similar items | Hidden de-bonding risks remain in stock |
How Did We Achieve Quality Improvement on Magnetic Silicone Balls by Installing Air Boosters and Tightening AQL?
Visual checks alone fail to intercept hidden de-bonding.
Without fixing pressure surges, adhesive defects recur continuously. Hardware pressure boosters and tightened sampling AQL standards provide dual-layer quality protection.
When producing Magnetic silicone balls, we installed air boosters on automatic dispensers to stabilize air pressure, achieving uniform glue output verified through a 50PCS trial run. Combined with IPQC first-piece checks and tightening AQL to MA:0.4 / MI:0.65, quality risks were eliminated completely.
5 Improvement Actions and AQL Tightening Verification Results
To resolve de-bonding and interception gaps, I led my team to execute five corrective actions.
First, upon receiving complaints, we conducted horizontal audits across similar inventory and recalled in-transit stock for sorting and rework.
Second, we installed an air booster on the automatic dispenser to ensure pressure stability and uniform glue output, verified via a 50PCS trial run with 0 defects.
Third, we documented this defect into a visual quality history board, using physical samples to train operators and inspectors for strict control.
Fourth, we instructed IPQC inspectors to treat seam de-bonding as a critical check during first-piece and patrol checks.
Fifth, we tightened OQC sampling AQL standards from MA:0.65 / MI:1.0 to MA:0.4 / MI:0.65.
Our raw materials comply with FDA Food Contact Regulations und RoHS Environmental Directives.
Our factory enforces quality controls under ISO 9001 Quality Standards.
| Improvement Verification Item | Detailed Engineering Standard & Specification | Actual Confirmation & Results |
|---|---|---|
| Dispenser Pressure Modification | Install air booster on automatic dispenser | 50PCS trial passed with 0 defects; 100% glue uniformity |
| Quality History Board Training | Mount physical sample boards; train staff on de-bonding | Inspector defect recognition improved; defense shifted |
| IPQC Process Inspection | Add seam peel force and glue starvation checks | Real-time bonding monitoring enforced; 0 batch defects |
| Tightened OQC Sampling | Tighten AQL from MA:0.65/MI:1.0 to MA:0.4/MI:0.65 | Defense line fortified; subsequent delivery 100% qualified |
In summary, stable dispenser air pressure and a strict OQC sampling defense line are vital to guarantee bonding quality. By adding air boosters and tightening AQL standards, we eliminated de-bonding defects permanently.
How to Specifically Operate Magnetic silicone balls?
When executing process optimization for Magnetic silicone balls, factories must follow standardized procedures. Third-party testing data shows that using pressure-boosted dispensing and compression molding with High-Temperature Vulcanized (HTV) silicone rubber combined with 200°C post-curing baking for 4 hours keeps dimensional tolerances within ±0.05 mm while outgoing AQL reaches MA:0.4 / MI:0.65 standards.
- Horizontal Stock Audit: Perform 100% visual and peel inspections across all similar bonded silicone inventory in stock and recall in-transit stock.
- Dispenser Booster Installation: Install an air booster on automatic dispenser feed lines and verify glue uniformity via a 50PCS trial.
- Quality History Board & Training: Mount defective physical sample boards to train production, IPQC, and OQC inspectors.
- IPQC Special Checks & AQL Tightening: Add seam peel tests during patrols and enforce OQC shipments under AQL MA:0.4 / MI:0.65.
External References & Industry Citations
- ISO 9001 Quality Certification: ISO 9001 Quality Management Systems Standard
- FDA Food Contact Regulations: U.S. FDA 21 CFR 177.2600 Food Contact Safety Regulations
- RoHS Environmental Directives: European Commission RoHS Directive 2011/65/EU
About Me and Dibo Tech
Brand Name: Dibo Tech Slogan: Dibo Technology Silicone Manufacturing Specialists Website: https://samxine.com/
Our Mission: Grounded in strong technical capability and quality, we specialize in custom OEM and ODM silicone rubber production, offering reliable custom solutions for our clients while fulfilling social responsibility for a sustainable future.
About Me: My name is Kunfa Ye, but my friends call me Jeff. I was born in 1986 under the sign of the Tiger. I started working in the silicone rubber manufacturing industry in 2014, and I now have fifteen years of experience. Over these years, I started from scratch and experienced every rise and fall in manufacturing. I know the hardships and rewards of entrepreneurship deeply. I always focus on professionalism and integrity in every project.
The silicone manufacturing industry seems ordinary, but it affects every part of industrial production. I know that trust stands behind every product, and trade relies on mutual success. Over the years, my proudest achievement is not achieving personal financial independence, but helping my clients optimize their supply chains and improve production efficiency. Their success brings me far more joy than personal achievements.
Now, I hope to give back to the industry—sharing experience, answering questions, and connecting resources. Whether you are a startup or an experienced industry peer, if I can help, I will do my absolute best. Because I always believe: the essence of business is the transfer of value, and true fulfillment comes from how much help you can bring to others.
Schreibe einen Kommentar